Components with complex geometries may contain both thick, solid sections and considerably thinner areas. This design affects how a component behaves during cutting, as different sections of the part do not have the same rigidity.
When CNC machining parts with significant variations in section thickness, the material removal strategy becomes particularly important. Proper clamping, a carefully planned sequence of operations and suitable cutting parameters help minimise deformation and maintain the required component accuracy.
Table of Contents
Why Are Variations in Section Thickness Challenging in CNC Machining?
Thicker sections of a component are generally more resistant to cutting forces, while thinner areas are more susceptible to deflection and deformation.
This becomes particularly important when large amounts of material are removed during CNC machining. As the geometry changes, so does the way the part responds to cutting and clamping forces. Therefore, process planning must take into account both the final component geometry and the changes occurring at successive production stages.
What Causes Deformation During CNC Machining of Such Parts?
Deformation can result from several factors, including material properties, changes in component rigidity, the clamping method and the sequence of machining operations.
As material is removed, the component’s behaviour during CNC machining also changes. Cutting parameters suitable for a solid workpiece blank may need to be adjusted at later stages of production.
Uneven Rigidity Across Different Sections
Differences in thickness cause individual sections of a component to respond differently to applied loads. This is particularly important when machining surfaces located near less rigid areas.
Excessive loads may cause temporary deflection, meaning that once the cutting force is removed, the surface may not achieve the intended geometry. Therefore, CNC machining preparation must account for the actual rigidity of individual sections of the component.
We discuss similar challenges related to deflection and vibration in our article “CNC machining of thin-walled parts – how to reduce vibrations and deformations?“.
Material Stresses and Changes in Geometry During Cutting
Removing material changes the distribution of internal stresses within the workpiece blank. In some cases, the release of these stresses may cause the component to change shape during production.
The risk may increase when significantly more material is removed from one section of the part than from others. The resulting uneven geometry further changes the rigidity of the entire component.
How to Plan CNC Machining of a Part with Varying Section Thickness
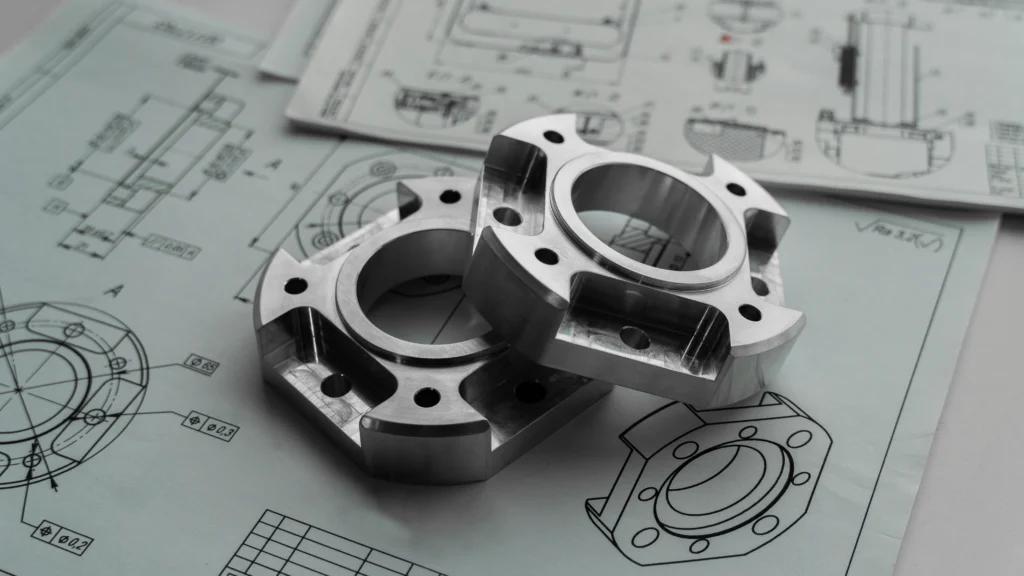
Process preparation requires consideration of the geometric changes that occur as material is removed. The sequence of operations and the stage at which surfaces with the tightest tolerances are machined are particularly important.
Our manufacturing facilities include more than 100 CNC machines, allowing us to select suitable equipment according to the component’s dimensions, geometry and requirements. For parts with varying section thicknesses, it is also essential to plan the process to maintain the stability of less rigid areas.
Material Removal Sequence
When section thickness varies significantly, the order in which material is removed from different areas matters. Removing too much material from one section too early may reduce the component’s rigidity before the remaining surfaces have been machined.
The sequence of operations should therefore maintain workpiece stability for as long as possible. A properly planned material removal strategy also reduces the risk of previously machined surfaces changing their position or shape during subsequent stages.
Separating Roughing and Finishing Operations
Dividing CNC machining into roughing and finishing stages allows most of the material to be removed first while leaving sufficient machining allowance to achieve the final dimensions.
After roughing, the component’s geometry is already closer to its final shape. If material removal has caused minor changes in shape, these can be taken into account during subsequent operations.
Finishing passes are used to achieve the required dimensions and surface quality, which is particularly important in areas with lower rigidity. We discuss this stage in more detail in our article “Surface finishing after CNC machining – what you need to know about the final stage of machining“.
How Does Clamping Affect Component Deformation During CNC Machining?
Clamping must keep the component stable during cutting without causing deformation. When section thickness varies, selecting appropriate support and clamping points is particularly important.
If clamping force is applied to a less rigid area, the component may be forced into a distorted position and partially return to its original shape once the clamping force is released. We therefore select clamping methods based on the geometry of the entire component and the changes in its rigidity during CNC machining.
How Do Cutting Parameters and Inspection Affect CNC Machining Accuracy?
Cutting forces depend, among other factors, on the tool used and the machining parameters. In less rigid sections of a component, excessive loads may cause deflection, vibration and reduced surface accuracy.
CNC machining parameters should be adapted to the material and the component’s geometry at each stage. Tool condition is also important, as a worn cutting edge can increase cutting forces and make it more difficult to maintain stable machining conditions.
Inspection of such components should cover both the required dimensions and the component’s geometry after the clamping force has been released. Measurements taken between successive operations allow deviations to be detected earlier and their impact on further production to be assessed.
At SIM Gdynia, we have more than 800 measuring instruments, allowing us to select inspection methods according to the component geometry and technical documentation requirements.
Summary
Significant variations in section thickness mean that different areas of a component may respond differently to cutting and clamping forces. When CNC machining such parts, the most important factors include the material removal sequence, dividing the process into appropriate stages, proper clamping and adjusting cutting parameters to the component’s changing rigidity.
Careful process planning helps reduce the risk of deformation and increases the likelihood of maintaining the required geometry of the finished component.
Do you need CNC machining for a component with challenging geometry? Contact us to discuss the available manufacturing options.